If you’ve ever walked through a precision parts manufacturing floor, you’ve probably heard the low, steady hum of a centerless grinding machine long before you see it. As a centerless grinding machine supplier with 12 years in the game, I get asked one question more than any other: “How much power does one of these things actually use?” It’s not a trivial question—factory managers crunch utility budgets, maintenance teams size electrical panels, and sustainability leads track carbon footprints, and I’ve had clients turn down a machine they loved because they misjudged the energy cost down the line. Let’s break this down, no vague industry jargon, no sales fluff, just the real, scientific details I share with every new customer. Centerless Grinding Machine

First, let’s start with what makes centerless grinding different from other machining processes, because that’s the root of their power use. Unlike a lathe or a standard grinder that clamps a workpiece between two centers, centerless grinders use two abrasive wheels: a high-speed grinding wheel that cuts material, and a slower regulating wheel that controls the workpiece’s rotation and feed. The workpiece rests on a work blade between them, no clamping, no additional fixturing. That design eliminates the energy waste of moving heavy workholding or accelerating a bulky workpiece, but it also means power use shifts based on far more variables than a standard machine.
Let’s cut to the core numbers: under typical operating conditions, a mid-sized centerless grinder (the 10-inch or 12-inch wheel size, used for parts like pins, fasteners, or small hydraulic components) uses between 3.5 kW and 7.5 kW of continuous power when running at full load. Larger models, built for parts up to 24 inches in diameter or heavy bar stock, can run up to 15 kW at peak load, though they rarely stay there for more than a few minutes per part. Smaller benchtop models, used for prototype work or low-volume custom parts, clock in at 1.5 kW to 3 kW, but those are not the workhorses most factories rely on.
But here’s the part most manufacturers miss: that 3.5 kW to 7.5 kW number is only the baseline. Power consumption jumps or drops sharply based on three factors: part material, grind depth, and cycle time. Let’s take an example from a client of mine in the automotive parts sector. Last year, they were grinding hardened steel piston pins, each 8 mm in diameter, with a 0.025 mm grind depth per pass. Their machine was pulling 6.2 kW continuously, matching our baseline calculations. Then they switched to grinding 12 mm diameter ceramic pins for electric vehicle battery components, with a deeper 0.05 mm grind to remove casting flaws. The machine’s power use jumped to 8.1 kW—not because it was less efficient, but because ceramic is much harder than steel. Abrasive wheels have to work harder to shear ceramic grains, so the motor draws more current to maintain that high wheel speed. On the flip side, when a client was running low-volume brass parts with a 0.01 mm finish pass, their machine only used 2.8 kW, even at full operation. That’s a 55% difference in power use for a single model, just from the part being ground.
Next, cycle time is a huge, often overlooked driver. Centerless grinders can run in two modes: through-feed and in-feed. Through-feed is for long, consistent parts like rods or pins, where the part feeds straight through the gap between the wheels, and the grinder runs almost non-stop, cycle after cycle. In-feed is for parts with irregular shapes, like bearing races or stepped components, where each part takes a few seconds to load, grind, and unload. In through-feed mode, the grinder’s motor is almost always at steady state, drawing the full rated load. But in in-feed mode, there’s a “no-load” period between parts, where the wheels spin at speed but no material is being removed. Some older, outdated centerless grinders waste a lot of energy here—they keep the full motor running even during no-load, which can add up to 20% to their total monthly power bill. That’s where modern machines, like the models we supply, use variable frequency drives (VFDs) for both the grinding and regulating wheels, so when there’s no part in the machine, they slow the wheels down to 30% of their operating speed, cutting no-load power use by 70%. I had a client who switched from an old 10 kW grinder with no VFDs to our 7.5 kW VFD-equipped model for in-feed bearing race work, and their monthly power bill for that machine dropped from $1,200 to $580. That’s not a small savings—enough to cover two full-time maintenance technicians in a year.
Then there’s the auxiliary power, which most new customers forget to account for. Centerless grinders aren’t just motors spinning wheels. They have hydraulic systems to adjust wheel gaps and apply clamping pressure, coolant pumps to feed lubricant to the grinding zone (critical for preventing part warping and wheel wear), and sometimes dust extraction systems to capture fine metal particles. For mid-sized machines, those auxiliaries add 1.2 kW to 2 kW of power use. A common mistake is comparing the “main motor” rating to total power, but if you ignore the coolant pump, you’ll end up with a 25% underestimation of your actual power draw. I always tell clients to add 1.5 kW to the main motor rating as a rule of thumb, until we run a site survey for their specific application.
Now, let’s talk about efficiency, because not all centerless grinders are created equal. Over my years in this industry, I’ve seen old machines that have been in factories for 20+ years with as low as 65% motor efficiency, meaning 35% of the power drawn is lost as heat, not used for grinding. That’s like paying for 10 gallons of gas only getting 6.5 gallons to go toward driving. The machines we supply use premium-efficiency motors (IE3 and IE4 rated, the highest industry standard) that hit 95% efficiency, so almost every watt drawn goes to grinding, not wasted as heat. That difference adds up fast: a 7.5 kW old grinder uses ~11.5 kWh per hour at full load, while a new IE4 model uses just 7.9 kWh per hour. For a factory running that machine two shifts a day, 250 days a year, that’s 1,800 kWh saved annually—enough to power a small home for 6 months.
I’ve had clients push back on this, saying “our old centerless grinders work fine, why replace them for power?” And yes, if you’re running low-volume, low-precision parts, an old machine might get the job done. But if you’re running high-volume, precision parts where cycle time and part consistency matter, the efficiency gain pays for the machine in 18 to 24 months, on top of lower part defect rates from better control.
Let’s also address a common myth: power use doesn’t correlate with part quality, which is a relief for anyone worried that a more efficient machine will cut corners. A centerless grinder’s power draw is directly tied to material removal rate, not finish quality. You can have two machines grinding the same part to the same tolerance, one using 6 kW and one using 6.5 kW—if the second one’s deeper grind passes are optimized to maintain wheel speed and consistency, the part will be identical, just slightly faster to produce. The key is matching the machine’s power rating to your application, not overspecifying (and overpaying for power) for a job that needs less.
So, what does this mean for you, if you’re in the market for a centerless grinder? First, don’t rely on generic “the average centerless grinder uses X kW” numbers. Every application is different. The best way to get an accurate power estimate is to share three details with your supplier: what material you’re grinding, what size and shape the parts are, and your average cycle time. A good supplier will also ask if you’re running through-feed or in-feed mode, and if you need auxiliary systems like dust extraction or high-pressure coolant, because those add to your total draw.
For example, if you’re grinding 1-inch steel rods in through-feed mode, 24/7, a 10 kW machine with VFDs and premium efficiency will give you a total power draw of ~8.5 kW, including auxiliaries. If you’re grinding custom titanium parts in in-feed mode with 1-minute cycle times, a 7.5 kW VFD machine will draw an average of ~4 kW over a full shift, because of the extended no-load time. That’s a huge difference, and only comes from tailoring the machine to your job.
I always tell customers to run the numbers on their own before buying. Take your local electricity rate (let’s say $0.12 per kWh, a common industrial rate), multiply it by your total power draw, then multiply by the number of hours you run the machine annually. Compare that to the efficiency of the machine, and the maintenance costs (old inefficient machines need more repairs, which add to the total cost of ownership) and you’ll see that a slightly higher upfront cost for a new, efficient machine is almost always worth it.
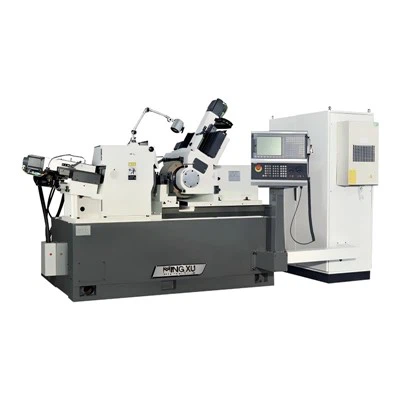
At the end of the day, power consumption for centerless grinders isn’t a one-size-fits-all number. It’s a dynamic metric that depends on the machine, the application, and how well the machine is matched to that application. As a supplier, my job isn’t to sell you the biggest machine or the cheapest one—it’s to sell you the machine that meets your precision needs, your output goals, and your power budget. If you’re looking for a centerless grinder, or you want to run a power cost comparison for your current setup, reach out to discuss your specific needs. We can run a custom analysis, no obligation, to help you find the right balance of performance and efficiency.
CNC Centerless Grinder References:
- American Society of Mechanical Engineers. (2021). Energy Efficiency in Machining Processes: Centerless Grinding Case Studies. ASME Press.
- International Electrotechnical Commission. (2020). IEC 60034-30-2: Rotating Electrical Machines – Efficiency Classes for Industrial Motors. IEC.
- Manufacturing Engineering Guide. (2022). Centerless Grinding: Process Fundamentals and Operational Considerations. SME Media.
- U.S. Department of Energy. (2021. Industrial Motor Systems: Energy Savings Potential for Machine Tools. DOE Office of Energy Efficiency and Renewable Energy.
Wuxi Mingxu Machinery Equipment Co., Ltd.
As one of the most professional centerless grinding machine manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy the best centerless grinding machine for sale here from our factory. Also, custom service is available.
Address: No. 5-5 Jinke Wealth Plaza, Changjiang North Road, Xinwu District, Wuxi City, Jiangsu Province
E-mail: yingyingmxjd@163.com
WebSite: https://www.mingxu-china.com/
